 You are here:
Rivet Nut vs Self-Clinching Nut: Appliance and Cabinet Guide - Full-Line
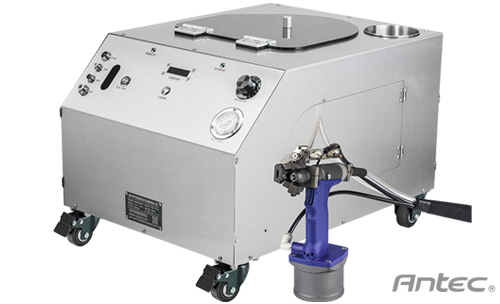
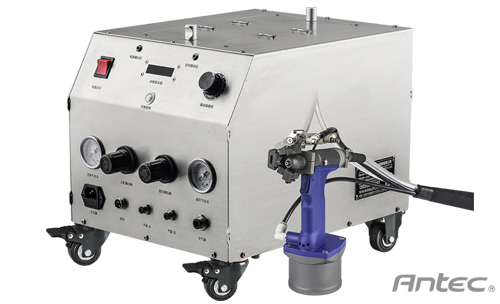
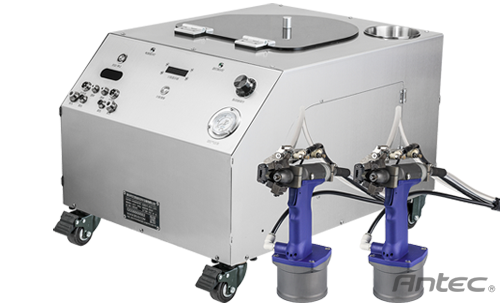
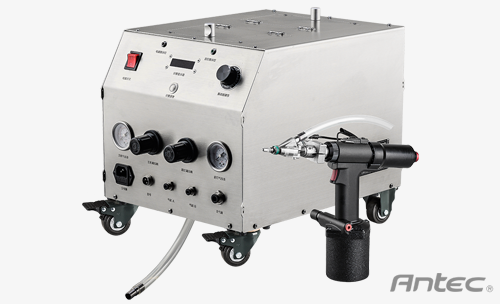
Appliance and cabinet shops keep coming back to the same question on thin sheet: rivet nut or self-clinching nut? Both create an internal thread in a thin panel, but the process, the equipment and the best use case differ sharply. Here is how they compare on the shop floor, and where a auto-feed rivet nut gun earns its place.
Because the working condition decides the machine, all three lines are developed in one factory and supported by one engineering team. The notes below look at auto-feed rivet nut gun work in that setting.
What manufacturing plants that rivet across several product types should remember: how the two processes differ; how to choose on the shop floor; sizing guidance; trial the auto-feed rivet nut gun, then fix the process.
1. How the Two Processes Differ
| Item | Rivet nut | Self-clinching nut |
|---|---|---|
| Forming method | Axial pull and cold forming with a auto-feed rivet nut gun | Radial press-in with a clinching press or punch press |
| Equipment | Handheld or auto-feed rivet nut gun, flexible | Needs a clinching press or die set, fixed station |
| Sheet thickness | Friendly to thin sheet, aluminum extrusion and irregular parts | Demanding on sheet thickness and hole consistency |
| Rework on site | Can be re-fitted in place after powder coating | Hard to rework once pressed wrong, needs dedicated equipment |
| Typical use | Cabinet doors, appliance panels, pallets | High-volume standard flat panels, pre-assembled chassis parts |
2. How to Choose on the Shop Floor
Appliances and kitchen equipment mean many variants, irregular parts and a lot of rework after powder coating, which suits the flexible rivet nut. Aluminum extrusion, battery trays and energy storage cabinets, meaning any structure that gets taken apart for service, also favor rivet nuts. For high-volume standard flat panels pre-assembled on a die-based line, the self-clinching nut is faster. Many plants run both: clinch the standard parts, rivet the irregular ones and the rework.
Across three lines, the fastest route is usually to match the working condition first and the model second.
3. Sizing Guidance
M3-M6 covers appliance thin-sheet panels, M6-M10 covers cabinet doors and mounting plates, and M10-M12 covers aluminum extrusion beams and trays; on aluminum parts use a knurled rivet nut rated for aluminum and verify with a pull-out test. Appliance solutions are on our appliance, kitchen and hardware furniture riveting page, cabinet solutions on the power distribution cabinet and electrical equipment page.
4. Trial the Auto-Feed Rivet Nut Gun, Then Fix the Process
When you are not sure, hand the part and the sheet thickness to an engineer and run one sample set with riveting and one with clinching, then compare forming, pull-out strength, appearance and rework cost before deciding. Antec can run a rivet nut sample at your plant; for general background see auto-feed rivet nut gun product overview.
Common Questions
Aluminum extrusion, irregular parts and structures that get disassembled usually favor the rivet nut; clinching is more demanding on the profile and the press, so confirm with a side-by-side trial.
Set a rivet nut into the prepared hole right through the coated part; it takes a few minutes and does not damage the finish.
Auto-Feed Rivet Nut Gun at a glance: 12,800 N pull force, 80 cycles per minute, in stock for fast delivery, response within 5 minutes.
Standard models ship from stock, custom builds are scheduled by project, and operator training is included after commissioning.
Which of the three lines fits this job?
Send the rivet specification and the workpiece drawing. Antec engineers will name the line, the model and the price band, then arrange a free on-site trial.
 Previous